

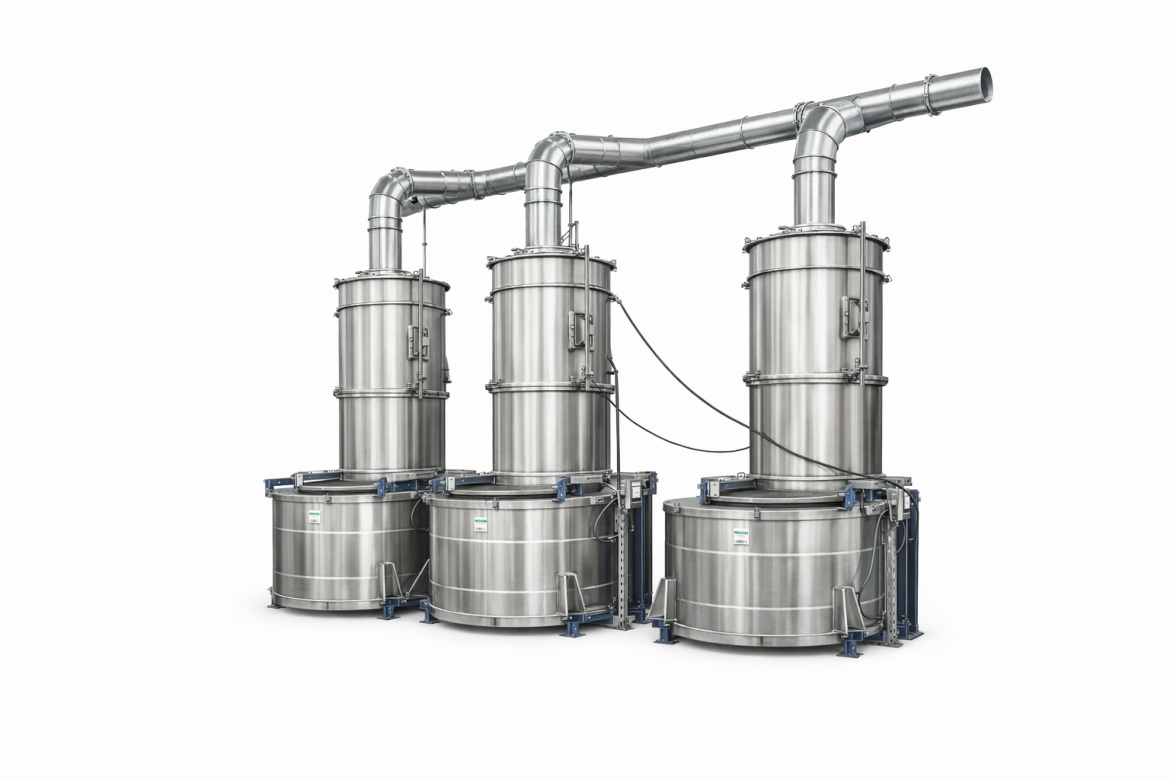
Innovative Aspiration Systems: Efficient Extraction Technology for Complex Industrial Demands
Modern industrial processes are scarcely conceivable without advanced aspiration systems. These solutions ensure clean, safe, and efficient workflows—from raw material handling to the secure processing of hazardous or sensitive substances. When dust, gases, or both occur together, only tailor-made concepts that integrate seamlessly into every operation provide genuine value.
The Path to the Optimal Solution for Every Production Environment
- Customized planning and engineering for specific requirements
- Precise extraction of dust and gases – from individual points to entire systems
- Consideration of ATEX directives for explosion protection
- Combined extraction concepts for complex material flows
- Efficiency gains through automated and semi-automated controls
Why Standard Solutions Often Reach Their Limits
Many industrial companies start with off-the-shelf solutions, which quickly reach their performance or safety limits in demanding environments. Special materials, process-specific conditions, or fluctuating parameters require systems that are flexible, scalable, and precisely matched to the application. Only with tailored technology can cycle times, product purity, and compliance with legal requirements be ensured over the long term.
Modern aspiration systems offer maximum flexibility with minimal interface. Planned from the ground up for each process, these solutions remain adaptable to future changes and expansions. The result is a system that meets not only today’s standards but is also ready for tomorrow’s challenges.
From Dust Extraction to Hybrid Solutions – Insights from Practice
Aspiration technology is more than just air filtration. Solutions range from spot extractions at problematic dust sources to channel extraction or hybrid systems that simultaneously capture and filter dust and gases. For explosion-prone zones (ATEX areas), detailed analysis and customized engineering are essential. The benefits: reduced wear, increased production safety, and significant cost savings thanks to minimized downtime.
One practical case: In a plant handling powdery raw materials, a fully automated aspiration system was implemented. It not only secures strict occupational and environmental standards but also reacts flexibly to frequent product changes. With intelligent sensors, throughput and cleanliness are dynamically balanced at all times.
ATEX Safety in Focus: Explosion Protection in Extraction Engineering
Explosion protection is a core element of modern aspiration system design. Solutions are realized in strict compliance with ATEX requirements—whether for dust, gas, or hybrid zones. Expert planning identifies all risk factors ahead of commissioning, delivering maximum safety and protecting both process and product quality.
Beyond ATEX conformity, factors such as noise reduction, ease of maintenance, and energy management are decisive. State-of-the-art aspiration systems are continually refined to maximize efficiency. The result: technologies that safeguard both people and the environment.
Project Planning: How Does a Tailor-made Aspiration System Emerge?
Every extraction project starts with an on-site assessment—essential for capturing processes and production conditions precisely. Next follows bespoke engineering focused on optimal airflow and energy saving. Innovative controls enable efficient monitoring, foreign substance detection, and flexible connection to up- and downstream systems. From planning to manufacturing and global installation, experienced experts manage the system’s entire lifecycle.
After commissioning, comprehensive service and maintenance ensure reliable, compliant, and long-lasting operation of the aspiration systems.
State-of-the-Art Technology for Sustainable and Secure Processes
The demands on modern industrial technology are rising—particularly regarding sustainability, resource efficiency, and operational reliability. Aspiration systems make a decisive contribution: they protect valuable raw materials, prevent product loss through carryover or build-up, and guarantee the highest product quality. Additionally, they minimize emissions, benefiting both the environment and staff.
Investing in made-to-measure aspiration solutions secures smooth operations, builds future-readiness, and strengthens competitiveness—regardless of industry or use case.